
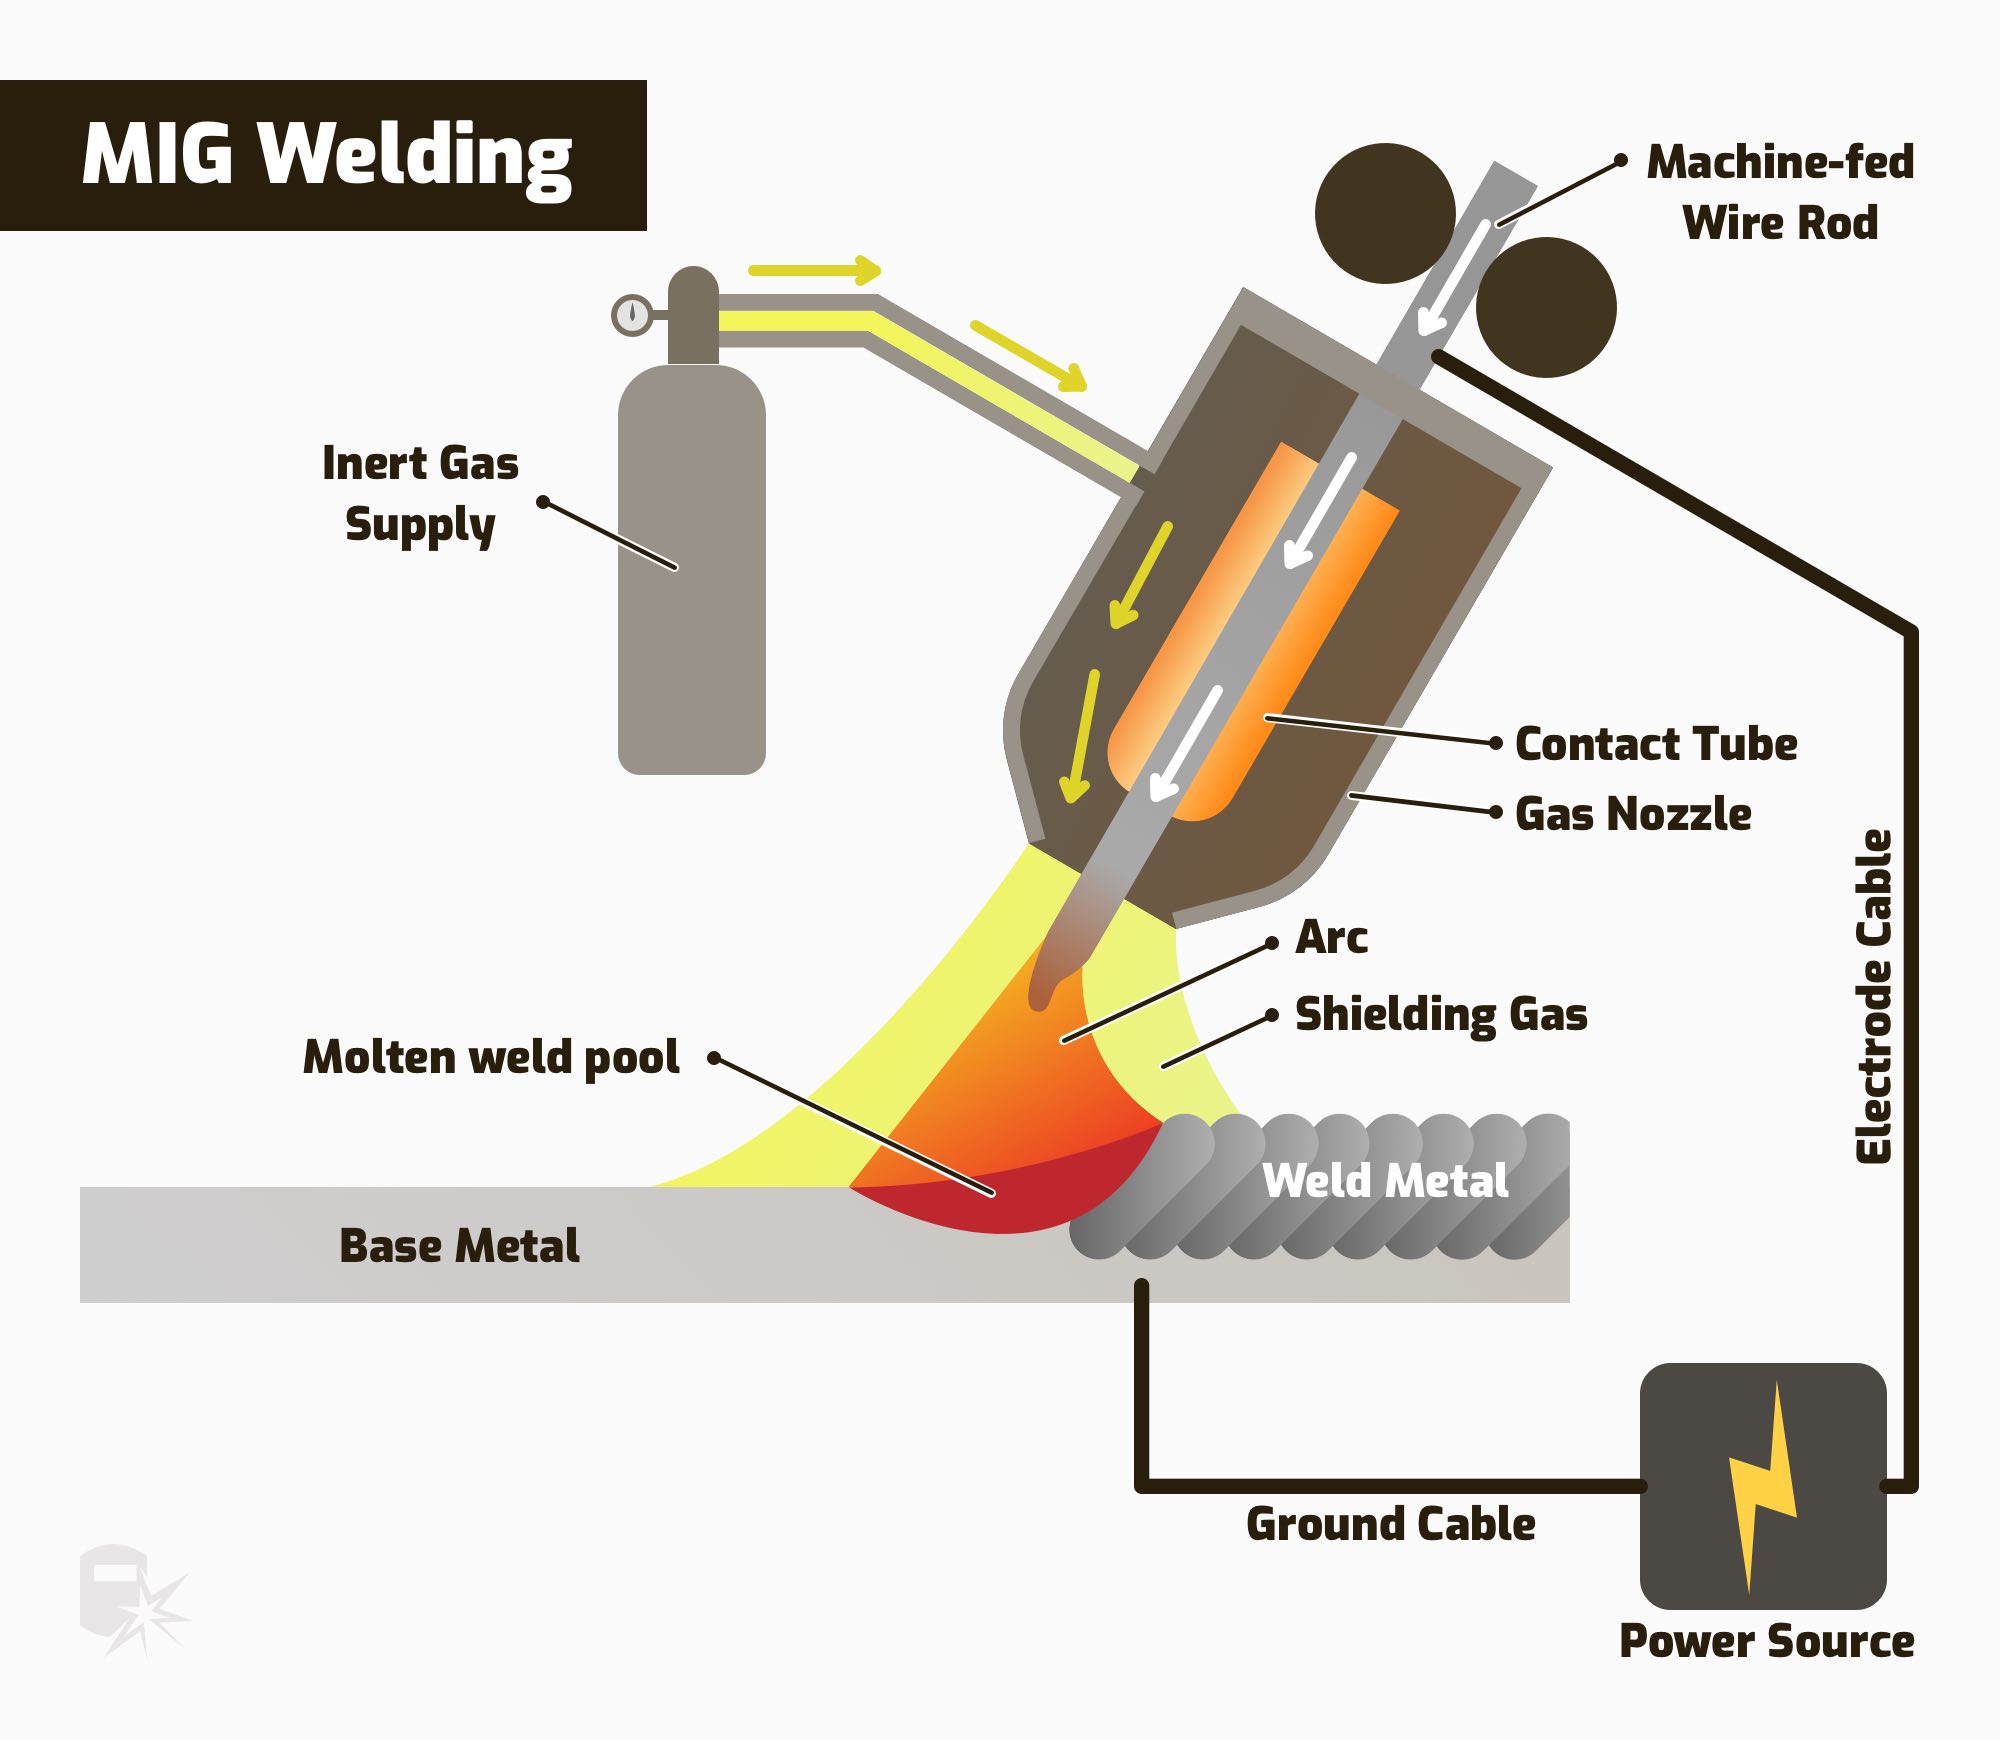
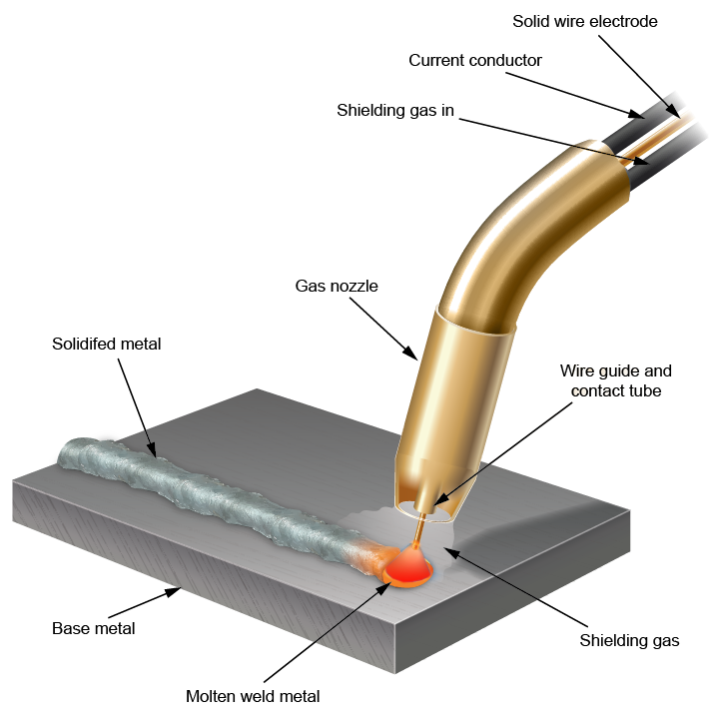
Gas Metal Arc Welding (GMAW), often recognized by its colloquial name, MIG welding (Metal Inert Gas), stands as a cornerstone technology in modern manufacturing and fabrication. It represents a sophisticated fusion process that has revolutionized the way metals are joined across countless industries, from automotive and construction to aerospace and robotics. At its heart, GMAW is an electric arc welding process where a continuous solid wire electrode is fed through a welding gun and into the weld puddle. Simultaneously, a shielding gas flows around the wire, protecting the arc and the molten weld pool from atmospheric contamination. The efficiency, versatility, and adaptability of GMAW make it a critical subject within the broader discourse of Tech & Innovation, particularly concerning advanced manufacturing techniques and the development of robust, reliable structures for complex technological systems.
Understanding the Fundamentals of Gas Metal Arc Welding
The operational efficacy of GMAW hinges on a meticulously orchestrated interplay of electrical, mechanical, and chemical principles. Unlike stick welding (SMAW) where the electrode is consumed and needs regular replacement, GMAW utilizes a continuously fed wire, significantly enhancing productivity.
The Arc and Wire Feed Mechanism
The core of GMAW is the electric arc generated between the continuously fed wire electrode and the workpiece. This arc provides the intense heat necessary to melt both the electrode wire and the base metal, forming a molten weld puddle that, upon solidification, creates a strong metallurgical bond. The wire, typically spooled, is fed through the welding gun at a precisely controlled speed by a motor-driven mechanism. This consistent wire feed ensures a stable arc and a uniform deposition rate, crucial for achieving high-quality welds. The arc initiation usually involves touching the wire to the workpiece, creating a short circuit, and then pulling it back slightly to establish a stable arc.
Shielding Gas: Protecting the Weld
A critical component of the GMAW process is the shielding gas. This inert or semi-inert gas, delivered coaxially with the wire electrode through the welding gun, forms a protective envelope around the welding arc and the molten weld pool. Its primary function is to prevent atmospheric gases—primarily oxygen and nitrogen—from contaminating the molten metal. Contamination can lead to porosity, cracking, and a significant reduction in weld strength and ductility. Common shielding gases include pure argon, carbon dioxide, or a mixture of both, with specific blends chosen based on the type of metal being welded and the desired weld characteristics. For instance, argon is excellent for aluminum, while argon-CO2 mixtures are favored for steel due to improved arc stability and penetration.
Power Sources and Polarity
GMAW typically employs a constant voltage (CV) power source. This means that for a given setting, the voltage remains relatively stable regardless of minor variations in arc length. The machine automatically adjusts the current (amperage) to maintain the preset voltage. This characteristic makes GMAW highly amenable to automation and easier for operators to control, as changes in wire stick-out (the length of the wire extending from the contact tip) only result in small changes in voltage, and the current adjusts to compensate. Direct Current Electrode Positive (DCEP), also known as reverse polarity, is the most common polarity used in GMAW. In DCEP, the electrode (wire) is connected to the positive terminal and the workpiece to the negative. This configuration provides deep penetration, a stable arc, and good bead characteristics, making it ideal for most applications.
GMAW as a Pillar of Modern Manufacturing Innovation
The evolution and widespread adoption of GMAW underscore its significance as a fundamental manufacturing innovation. Its inherent characteristics align perfectly with the demands of contemporary industries that prioritize speed, efficiency, and consistent quality in fabrication.
Versatility Across Materials and Applications
One of GMAW’s most compelling attributes is its remarkable versatility. It is highly effective for welding a wide array of ferrous and non-ferrous metals, including carbon steel, stainless steel, aluminum, magnesium, and copper alloys. This broad material compatibility means that a single GMAW setup can be adapted for diverse applications, from joining thin sheets in automotive body construction to fabricating thick structural components in shipbuilding. Its ability to handle different material thicknesses and joint configurations makes it an indispensable tool in workshops and factories globally, allowing for streamlined production lines and reduced equipment overhead.
Automation and Robotics in GMAW
The continuous wire feed and constant voltage characteristics of GMAW make it exceptionally well-suited for automation and robotic integration. Robotic GMAW systems are now commonplace in high-volume manufacturing environments, offering unparalleled precision, repeatability, and speed. Robots can execute complex weld paths with extreme accuracy, minimizing human error and ensuring consistent weld quality across thousands of identical parts. This automation not only boosts productivity but also improves worker safety by removing operators from hazardous welding environments. The integration of advanced sensors and control systems further enhances robotic GMAW, allowing for real-time adjustments and adaptive welding, marking a significant stride in manufacturing innovation.

Efficiency and Productivity Gains
Compared to other welding processes, GMAW offers superior efficiency and productivity. The continuous wire feed eliminates the need for frequent electrode changes, reducing downtime and increasing arc on-time. High deposition rates, meaning the amount of weld metal deposited per unit of time, translate into faster welding speeds and quicker completion of projects. Furthermore, the relatively low spatter generation of GMAW reduces post-weld cleaning, contributing to faster overall production cycles. These efficiency gains are critical for industries operating under tight deadlines and cost pressures, making GMAW an economically advantageous choice for many manufacturing challenges.
Advantages and Limitations in High-Precision Fabrication
While GMAW offers significant benefits, understanding its inherent advantages and limitations is crucial for its optimal application, especially in contexts demanding high precision and specific material properties.
Speed and Deposition Rates
The defining advantage of GMAW is its remarkable speed and high deposition rate. The continuous wire feed and stable arc allow for rapid welding, significantly shortening production times. This makes it ideal for large-scale production runs and for fabricating components where speed is a primary concern without compromising structural integrity. In an era where technological advancements often hinge on rapid prototyping and quick market deployment, GMAW’s speed offers a competitive edge in manufacturing complex assemblies.
Quality Control and Skill Requirements
GMAW is known for producing aesthetically pleasing welds with good penetration and minimal defects, provided the parameters are correctly set. However, achieving consistent high-quality welds still requires a skilled operator, especially for manual applications. While automated systems mitigate some of this, proper machine setup, gas selection, wire speed, and voltage adjustments are paramount. Poor technique or incorrect parameters can lead to issues such as lack of fusion, porosity, or undercut, underscoring the importance of meticulous quality control and skilled craftsmanship or advanced robotic programming.
Portability and Environmental Considerations
Compared to other processes like submerged arc welding, GMAW equipment can be relatively portable, making it suitable for fieldwork and smaller workshops. However, the need for shielding gas tanks limits true mobility compared to processes that do not require external gas. Environmentally, while GMAW produces less fumes and slag than some other methods, proper ventilation is still essential to protect workers from welding fumes, which can contain harmful particulates. Innovations in fume extraction and personal protective equipment continue to address these environmental and safety concerns.
Future Trends and Innovations in GMAW Technology
The field of GMAW is not static; it is continually evolving through research and development, integrating cutting-edge technologies to enhance its capabilities and broaden its applications within the realm of Tech & Innovation.
Sensor Integration and Adaptive Welding
Future GMAW systems are increasingly incorporating advanced sensor technologies. Vision systems, laser scanners, and thermal cameras are being integrated to monitor the weld puddle in real-time, providing critical data on bead geometry, temperature, and penetration. This data feeds into intelligent control systems, enabling adaptive welding where parameters like wire feed speed, voltage, and torch angle can be adjusted dynamically during the welding process. This “smart welding” capability ensures optimal weld quality even when facing variations in material thickness, joint fit-up, or environmental conditions, pushing the boundaries of precision manufacturing.
AI and Machine Learning in Weld Optimization
The vast amounts of data generated by advanced GMAW systems are ripe for analysis by artificial intelligence (AI) and machine learning (ML) algorithms. AI can be trained to recognize weld defects, predict potential issues, and even suggest optimal welding parameters based on material properties, joint type, and desired outcomes. Machine learning models can analyze past successful welds to continuously refine processes, identify patterns that lead to superior results, and even automate troubleshooting. This AI-driven approach is set to revolutionize quality control, process efficiency, and the development of new welding applications, transforming GMAW into a truly intelligent manufacturing process.
Advanced Materials and Hybrid Processes
As industries demand lighter, stronger, and more specialized materials, GMAW technology is adapting. Research is ongoing to optimize GMAW for welding advanced high-strength steels, exotic alloys, and composite structures. Furthermore, hybrid welding processes, combining GMAW with other techniques such as laser welding, are gaining traction. These hybrid methods leverage the strengths of each process—for example, the deep penetration of laser welding with the gap-bridging capability of GMAW—to achieve superior weld characteristics, faster speeds, and greater efficiency for complex fabrication challenges. These innovations will enable the creation of more robust and sophisticated components for next-generation technologies across various high-tech sectors.