
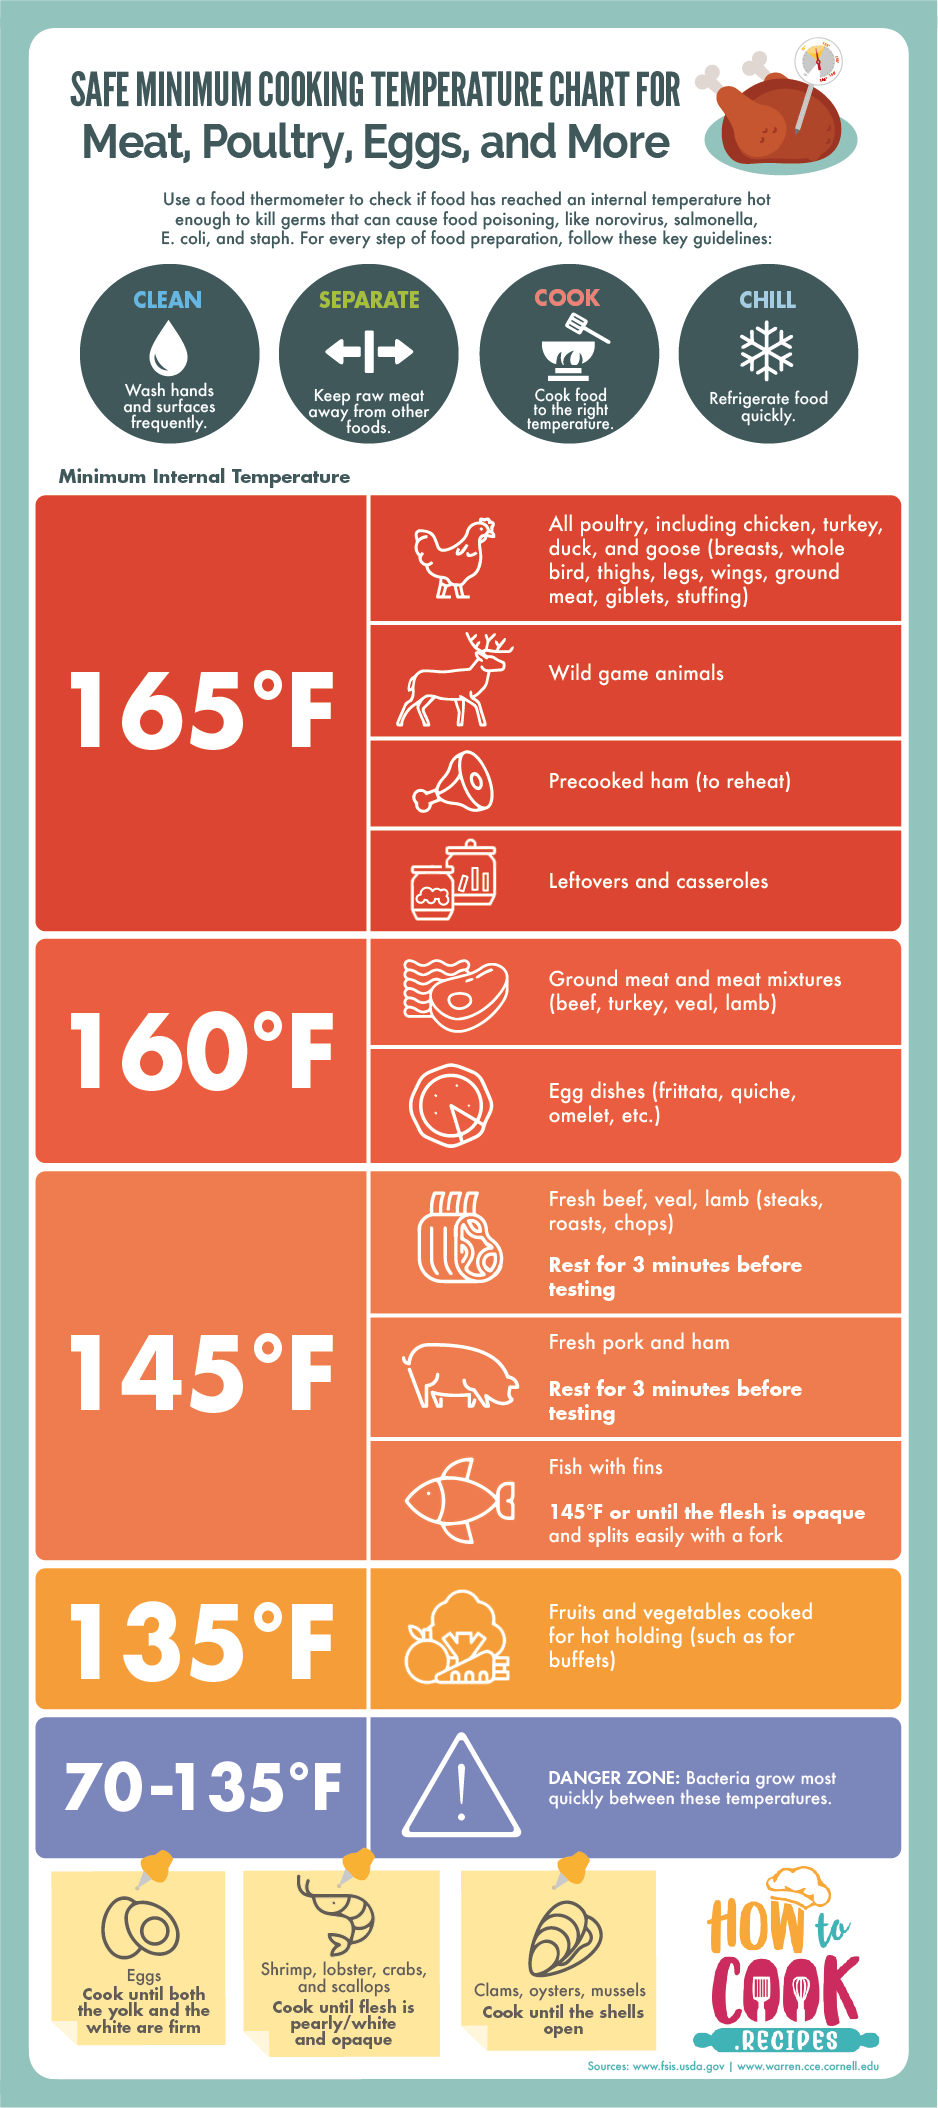
The question “what is internal temperature of cooked chicken” transcends a simple culinary inquiry, evolving into a critical challenge for industrial food processing plants. Ensuring that every piece of poultry reaches and maintains the precise internal temperature required for food safety and optimal texture is a monumental task, given the scale of modern production. This complex problem, pivotal for public health and product quality, has become a fertile ground for innovative solutions rooted in advanced Tech & Innovation, particularly leveraging AI, autonomous flight systems, and sophisticated remote sensing capabilities. Far beyond a kitchen thermometer, the industrial pursuit of thermal uniformity drives the integration of cutting-edge technologies aimed at revolutionizing quality control, predictive analytics, and process optimization within poultry processing.
The Imperative of Thermal Uniformity in Industrial Food Processing
Achieving a consistent and safe internal temperature across vast batches of cooked chicken is a non-negotiable aspect of industrial food production. Any deviation can lead to health risks from undercooked products or compromised quality from overcooking. For producers operating at scale, the objective is not merely to know the temperature, but to guarantee it uniformly across millions of units, a task that traditional, manual spot-checking methods struggle to accomplish with the required precision and efficiency. The underlying challenge demands a systemic approach, where every stage of cooking, from initial heat application to final cooling, is meticulously monitored and controlled.
Current Challenges in Large-Scale Temperature Verification
Traditional temperature verification methods in industrial kitchens often rely on periodic manual probes or fixed in-oven sensors, which provide localized data points. These methods, while essential, inherently offer an incomplete picture of the thermal landscape within massive industrial ovens or cookers. Hot spots, cold zones, and uneven heat distribution can lead to significant variations in internal temperatures that go undetected, compromising food safety standards or leading to product waste. The sheer volume and speed of production further complicate comprehensive real-time monitoring, creating data gaps that manual intervention cannot adequately fill. Moreover, the human element introduces variability, making a truly consistent and unbiased assessment difficult to sustain over long shifts. The need for a more dynamic, comprehensive, and automated verification system is paramount for addressing these inherent limitations and ensuring unparalleled product integrity.
The Role of Predictive Modeling and AI in Cooking Consistency
To overcome the limitations of reactive measurement, the food industry is increasingly turning to predictive modeling and artificial intelligence. AI algorithms, trained on vast datasets encompassing oven temperatures, cooking times, poultry size and density, and historical temperature probe data, can develop sophisticated models that predict internal temperatures with remarkable accuracy. These models can anticipate potential deviations before they occur, allowing for proactive adjustments to cooking parameters. Machine learning systems can continuously learn from new production cycles, refining their predictions and optimizing cooking profiles to minimize variability. For instance, an AI might analyze real-time air flow patterns and product distribution within an oven to suggest precise adjustments to conveyor speed or heat settings, ensuring that every chicken piece achieves its target internal temperature simultaneously. This shift from reactive error correction to proactive process optimization represents a fundamental transformation in quality assurance, driven by intelligent systems that continuously strive for thermal perfection.
Drone-Based Remote Sensing for Process Monitoring
The application of drone technology, traditionally associated with aerial mapping or surveillance, is finding innovative traction within the confined yet expansive environments of industrial food processing plants. Equipped with advanced sensor payloads, drones can offer a new dimension of remote sensing capabilities, providing unparalleled aerial perspectives and data collection opportunities that are impractical or impossible for static sensors or human operators. Their mobility and ability to navigate complex industrial layouts make them ideal candidates for comprehensive, non-invasive process monitoring, specifically targeting thermal distribution and other critical parameters within large-scale cooking operations.
Integrating Thermal and Multispectral Imaging in Food Production

A key innovation in this field is the integration of thermal and multispectral imaging systems onto autonomous drones. Thermal cameras can detect surface temperature variations across large batches of poultry as they move through ovens or cooling zones. While thermal imaging provides surface data rather than direct internal temperature, AI models can correlate specific surface thermal signatures with predicted internal temperatures, especially when combined with other data inputs. Multispectral cameras, on the other hand, can analyze variations in spectral reflectance, potentially identifying changes in product composition or cooking progression that are not visible to the naked eye. By flying over cooking lines or storage areas, drones can collect continuous, high-resolution thermal and multispectral data, mapping temperature gradients and identifying anomalies that could indicate uneven cooking or potential spoilage risks. This comprehensive data stream feeds directly into AI analytics platforms, providing a holistic view of thermal uniformity and product state across the entire production line.
Autonomous Flight Paths for Comprehensive Plant Surveillance
The deployment of drones within industrial facilities requires sophisticated autonomous flight capabilities. Programmed with precise flight paths, these drones can navigate complex interior environments, avoiding obstacles, and maintaining optimal distances for sensor operation. Autonomous flight ensures consistent data collection, repeatable surveys, and minimizes human error. For large-scale poultry operations, drones can be configured to execute predefined routes over conveyor belts, oven exits, and chilling tunnels, performing continuous scans. Equipped with real-time obstacle avoidance and precise localization systems, these UAVs can operate safely alongside existing machinery, collecting vital data points without disrupting production flows. This systematic approach to plant surveillance enables continuous monitoring of thermal performance, identifying localized hot or cold zones that might indicate equipment malfunction or uneven processing, thus ensuring that every product batch adheres to the strictest thermal guidelines.
AI-Driven Analytics for Enhanced Quality Assurance
The sheer volume of data generated by drone-based remote sensing—from thermal maps to multispectral signatures and flight telemetry—would be overwhelming without advanced analytical capabilities. This is where AI plays an indispensable role, transforming raw data into actionable insights that drive enhanced quality assurance and operational efficiency. The integration of machine learning algorithms allows for rapid processing, pattern recognition, and predictive modeling, creating a responsive and intelligent quality control ecosystem.
Real-time Data Interpretation and Anomaly Detection
AI algorithms are designed to sift through vast datasets from drone sensors in real-time, identifying patterns, trends, and anomalies that human operators might miss. For instance, a persistent localized cold spot in a thermal map of a chicken batch exiting an oven could signal a malfunctioning heating element or an airflow obstruction. AI can detect such deviations instantly, trigger alerts, and even suggest corrective actions, such as adjusting oven settings or scheduling maintenance. Machine learning models can be trained to recognize specific thermal signatures associated with optimal cooking, undercooking, or overcooking, providing immediate feedback on product quality. This real-time data interpretation moves quality control from a post-production inspection model to an in-process, preventative one, ensuring that issues are addressed as they arise, minimizing waste, and maximizing product consistency. The ability of AI to learn and adapt means that its detection capabilities continuously improve with more data, making the system increasingly robust and reliable.
Future Implications: Towards Fully Automated Quality Control
The trajectory of this technology points towards increasingly automated quality control systems. Imagine a future where autonomous drones continuously monitor every stage of poultry processing, from raw material inspection to final packaging. AI systems will not only detect anomalies but will also autonomously trigger corrective actions, adjusting machinery parameters, rerouting product batches, or even flagging individual items for closer inspection based on their unique thermal and spectral signatures. This level of automation, powered by AI and advanced remote sensing, promises to drastically reduce human error, improve response times, and achieve an unprecedented level of consistency in product quality and safety. The insights gained from continuous, granular data analysis will also fuel further innovation in equipment design and process optimization, pushing the boundaries of what is achievable in industrial food production.
The Evolving Landscape of Food Safety Technology
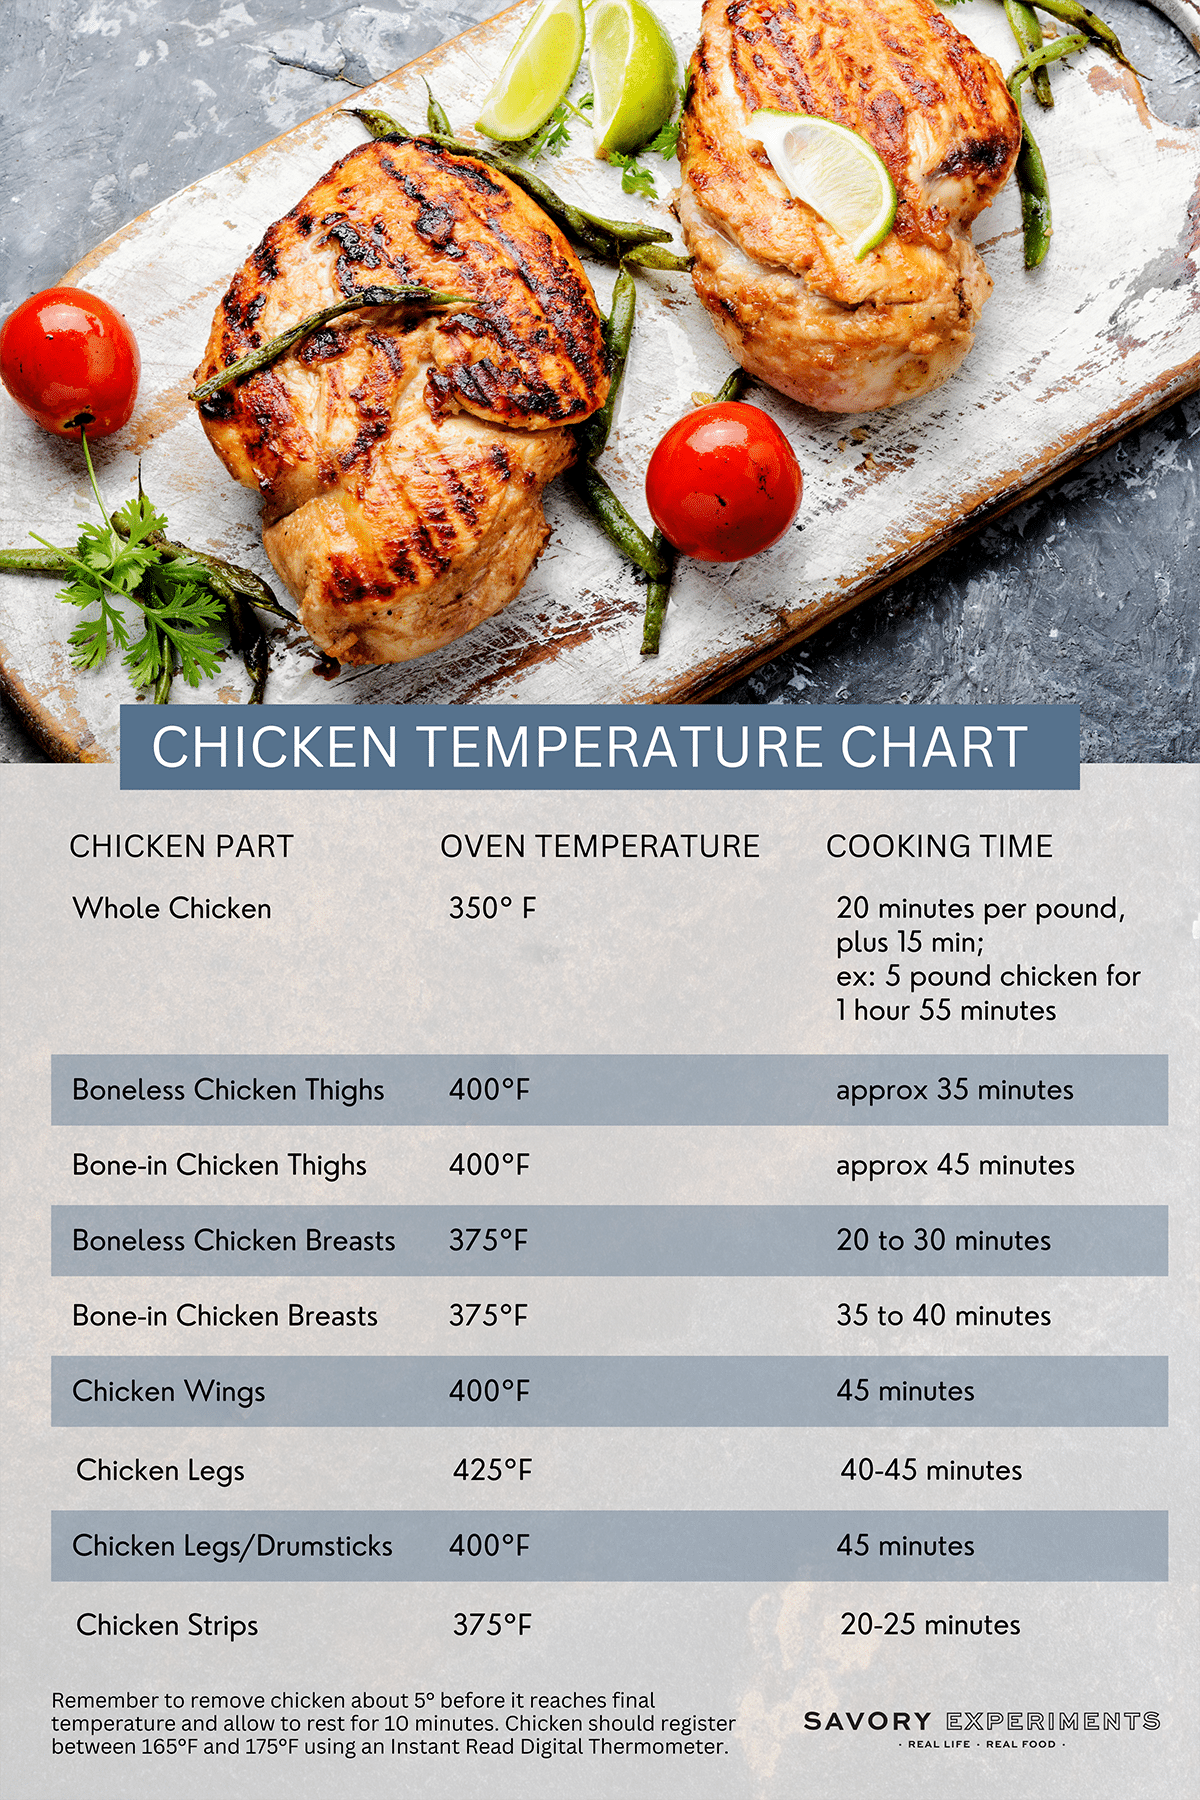
The seemingly simple question of “what is internal temperature of cooked chicken” expands into a complex domain of advanced technological application when scaled to industrial production. The deployment of AI, autonomous drones, and sophisticated remote sensing in food processing plants is not merely an incremental improvement; it represents a paradigm shift in how food safety and quality are managed. By providing comprehensive, real-time, and predictive insights into thermal uniformity and product state, these technologies are setting new benchmarks for efficiency, consistency, and consumer safety. As these innovations mature, the industrial kitchen will become an increasingly intelligent environment, where the precise internal temperature of every cooked chicken product is not just measured, but guaranteed through a symphony of interconnected, intelligent systems. This evolution underscores the critical role of Tech & Innovation in safeguarding public health and enhancing the global food supply chain.